
- ISO 9001:2015 / IATF 16949:2016 / ISO 14001:2015, certificate numbers published and verifiable.
- Build-to-print work: the plant cuts to your design and reports against your drawing.
- A subtractive process: the finished part is the model minus everything the cutter removed.
- Three linear axes (X / Y / Z), the tool moves, the part stays put for a setup.
- Cost is decided at the manufacturability review, before the first chip.
- No minimum order — prototype and production run on the same machines.
What the three axes actually do
A 3-axis machine holds the workpiece fixed, typically in a vise or on a fixture, and moves the cutting tool along three perpendicular linear axes: X (left–right), Y (front–back), and Z (up–down). The spindle approaches the stock from above and cuts any feature it can reach with a straight plunge and a side pass.
That geometry has a hard edge. A pocket, a hole pattern, a flat face, and a 2D profile are all straightforward, because the tool can see them from above. But a feature on a side wall, or one that sits at an angle to the table, cannot be reached without either flipping the part to a second setup or adding rotary axes (4-axis / 5-axis) to present it to the cutter.
The practical limit of 3-axis work is tool access, not the metal. That single fact explains most "can this be done on a 3-axis?" conversations: if a cutter can get to the surface, it can be cut; if not, the part needs more setups or more axes. The design then becomes a CAD model, which CAM software turns into toolpaths, which the controller runs as G-code — the same chain whether the part is one-off or ten thousand.
In practice "3-axis" describes the feature set as much as the axis count. The work it does best is prismatic — flat faces, straight walls, pockets, and holes — and the large majority of it is what shops call 2.5D: every cut is either a flat bottom or a profile reachable from above. True 3D contouring (sculpted surfaces) is possible, but it is slower and less accurate than on a 5-axis machine, so it is the exception rather than the rule.
Buyer action: before requesting a process, note which faces carry the features that matter. If they all face up or lie in one or two planes, 3-axis is the natural home. If they wrap around the part, write that down — it changes the conversation from "can it be done" to "how many setups".
When 3-axis is enough, and when it isn't
This is the question that actually saves money, and it is worth answering before any process is chosen:
- 3-axis is enough when the part is essentially prismatic — plates, blocks, housings — and its features face one or two setups. Most brackets, enclosures, and fixtures fall here.
- 3-axis is not enough when the part has undercuts, side-wall features at an angle to the table, or geometry that needs simultaneous access from several directions. Those need a rotary axis (4 / 5-axis) or one or more extra setups.
- The honest middle: many parts quoted as "5-axis" are really 3-axis parts with one extra setup. The real choice is whether the extra setup costs more than the extra axis. And on a well-fixtured prismatic part, the setup usually wins.
Geometries that fit 3-axis well
- Blocks and plates — fixture plates, baseplates, mounting rails, heat sinks.
- Brackets and adapters — L-brackets, flanges, clamping jaws, sensor mounts.
- Housings and enclosures — boxes with accessible internal pockets, covers, panels.
- Jigs, fixtures, and tooling components — anything essentially flat with holes and pockets.
Geometries that do not fit 3-axis (or fit it badly)
- Undercuts — features a straight tool cannot retract from without colliding.
- Compound-angle surfaces — faces tilted in two axes relative to the table.
- Free-form 3D — turbine blades, impellers, organic surfaces.
- Very tall aspect ratios — long thin walls and deep narrow cavities that chatter or distort.
| Axis count | What it adds | Best for | Setup cost |
|---|---|---|---|
| 3-axis | Tool moves in X/Y/Z; part fixed per setup | Prismatic parts, pockets, hole patterns, plates | Lowest; one or two setups |
| 4-axis | Adds one rotary (A or B) — rotates the part | Cylindrical features, side faces, indexable angles | Low–moderate |
| 5-axis | Adds two rotary axes — tilts and rotates | Compound angles, free-form 3D, undercuts in one setup | Higher machine rate, fewer setups |
Where 3-axis earns its keep: industrial automation brackets, electronics enclosures, agricultural and construction hardware, medical device housings (build-to-print, non-sterile), automotive jigs and fixtures, and robotics end-effectors. It is the default wherever the part is essentially flat, the volume is low-to-mid, and the material must be metal or a certifiable plastic.
How does the work actually move through the shop?
The sequence is quoting and manufacturability review, programming and offline verification, fixturing, roughing, finishing, inspection, and first-article reporting. Each stage has a way to fail, and the expensive ones are the first and the last.
Cutting is usually the shortest part of the calendar time. Queue position, fixture design, and inspection documentation account for most of the lead, which is why asking for the first-article date and the repeat date separately gives a truer picture than a single lead-time number.
Where 3-axis sits in the process chain matters more than buyers expect. It is the middle of three subtractive families: turning owns round, rotationally symmetric parts (shafts, bushings, fittings); 3-axis milling owns prismatic blocks and plates; 4/5-axis owns the parts that turning and 3-axis cannot reach. A part is usually assigned to one of these by its dominant geometry, not by preference — mixing them (mill-turn) is for parts that are partly round and partly prismatic.
Buyer action: state the dominant shape in the RFQ. "Round bar, one flat milled face" routes to turning with a secondary op; "solid block, pockets both sides" routes to 3-axis. Getting the family right is the first cost control.
Four questions that expose a 3 axis CNC machining reseller
These four checks cost nothing and can be run before any commitment.
- Can they name the registration number? Ours is 91441900MA4UWT6X39. Check it in the National Enterprise Credit Information Publicity System.
- Do they name machine families and counts? A manufacturer lists models; a reseller recycles stock photos.
- Are the certificate numbers verifiable? Real ISO/IATF certificates carry numbers you can confirm with the registrar.
- Can you walk the floor? On-site and video audits are welcome at the Dongguan address.
What to do with the answers: a real manufacturer answers all four without hesitation and will name the machine models on the floor. If the registration number comes back as a trading licence, or the certificate numbers cannot be tied to a registrar, treat the quote as a resale and price the risk of a broken chain accordingly.
What design decisions move the cost on 3 axis CNC machining?
Three design decisions drive most of the cost on a machined part: internal corner radii matched to a real cutter diameter, cavity depth kept within about four times the tool diameter, and a general tolerance on every feature that does not mate. Each one changes the tool that can be used, and the tool determines how much material can be removed per minute, which is why these matter more than any process selection.
This is worth raising at quote stage rather than after the first article, because the changes are usually trivial on the drawing and significant on the machine.
A practical DFM checklist for 3-axis parts:
- Internal corner radius ≥ the smallest tool you can accept — a 1 mm corner needs a 1 mm cutter that is slow and fragile; opening it to 3 mm lets a stiffer tool run.
- Cavity depth ≤ ~4× tool diameter — deeper cavities need long, whippy tools that chatter and must be run slowly.
- Wall thickness ≥ 0.8–1.0 mm in metal — thinner walls flex, vibrate, and distort on release.
- One general tolerance for non-mating features — tight callouts on every dimension inflate inspection, not function.
- Accessible datums — pick flat, reachable surfaces as A/B/C so the part seats repeatably.
None of these change the design's function; all of them change the cycle time and the inspection load. Raise them at quote stage, not after the first article.
Who is on the other side of the purchase order?
Legally this is Dongguan Zhuohang Ltd, established 2005, Social Credit Code 91441900MA4UWT6X39, operating under the name Zhuohang Precision Machining Factory from No. 8, Shuibian Songyuan Road, Hengli Town, Dongguan, Guangdong, China 523470.
The 18-character code, checked against the National Enterprise Credit Information Publicity System, confirms a real manufacturer. A trading company may hold a business licence as well, but its scope is trading, not manufacturing, and its address is an office rather than a plant.
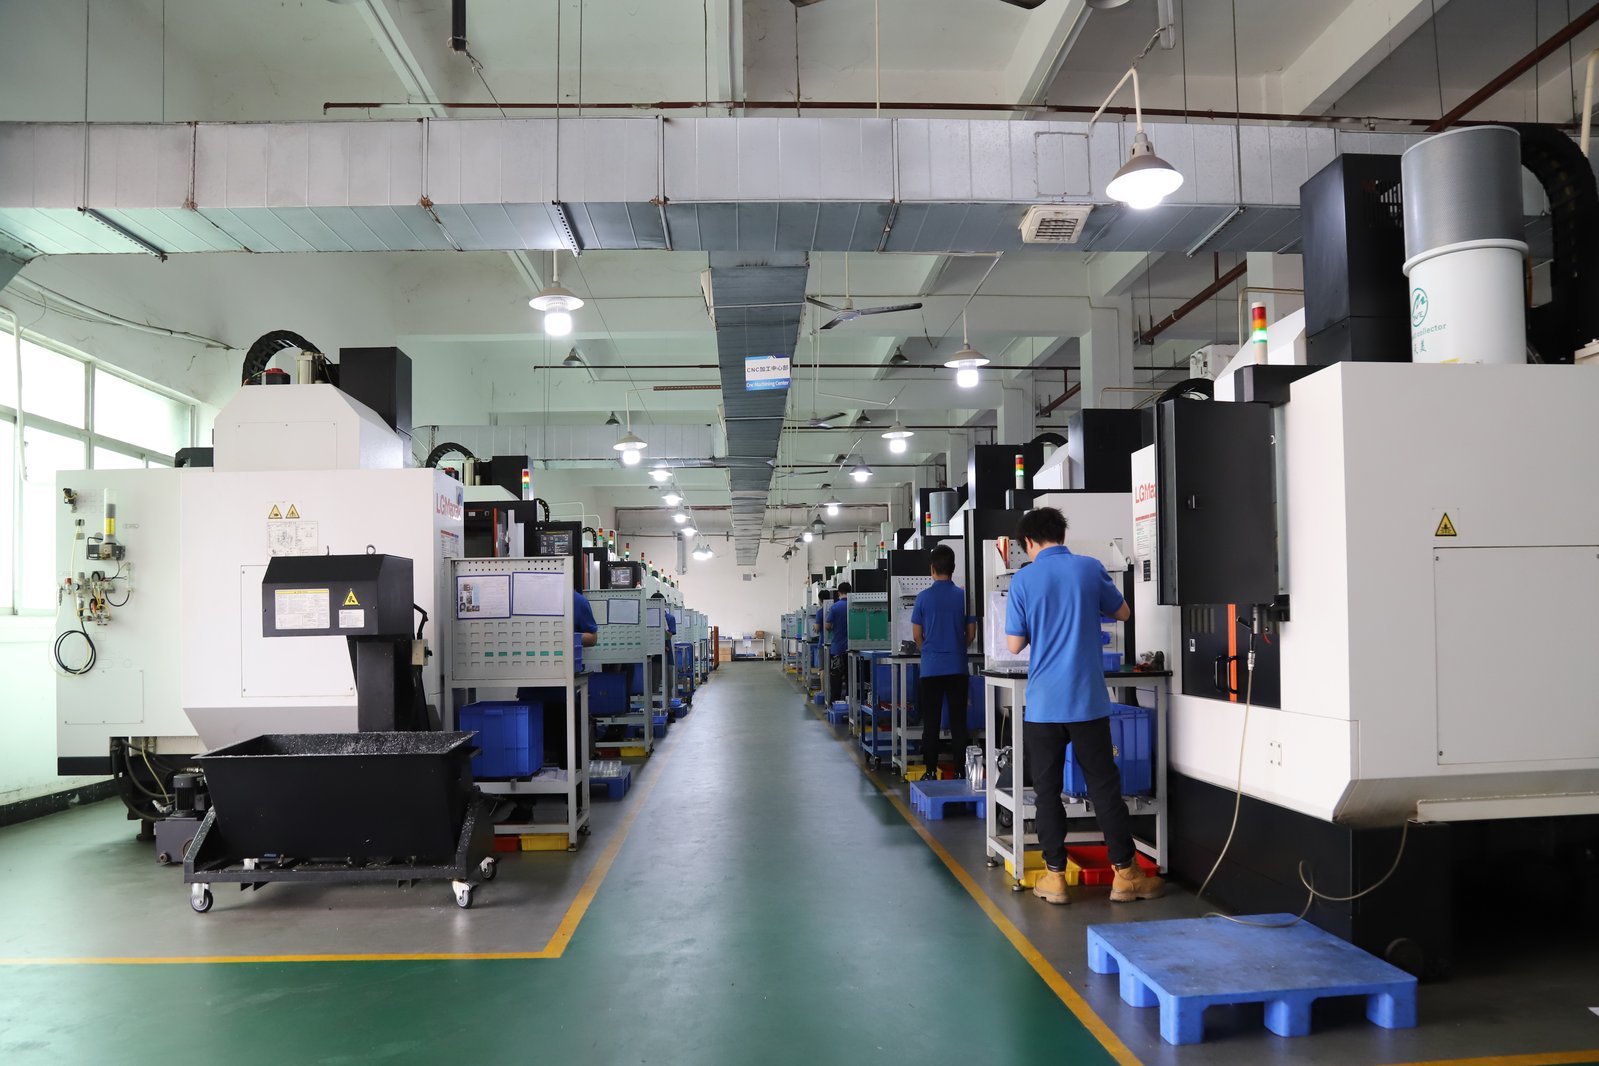
The operation behind the name is a manufacturer, not a trading desk: a 6,800 m² plant in Hengli, Dongguan, running 100+ CNC machines with a staff of 100+. The business was registered in 2005, and the 18-character Social Credit Code — 91441900MA4UWT6X39 — is the single fact that separates a plant you can audit from a reseller you cannot. A trading company holds a licence too, but its scope line reads "trade", and its address is an office, not a machine floor.
What capacity sits behind this?
Total machine count is not the question. The question is how many machines sit in the family that makes your part, because that is the queue your part waits in. The floor runs over a hundred machines: 50+ three-axis centres for prismatic work, 20+ four-axis, 20+ five-axis, 25+ turning and mill-turn centres, Swiss-type lathes for long slender parts, precision grinding and wire EDM for the tightest features.
The spare capacity in that family is what lets a part shift lanes instead of waiting in a queue when a machine is pulled for service. That, not the headline machine, is what protects a delivery date.
The machine families behind that count are named, not anonymous: Mazak, Brother, TSUGAMI, Sodick, STAR, and CITIZEN across machining centres, turn-mill, wire EDM, and Swiss-type lathes. Naming the families matters because spare depth in the family that makes your part is what protects a delivery date when a machine is pulled for service — the part shifts lanes instead of waiting in a queue.
How does the process actually run, step by step?
The sequence is quoting and manufacturability review, then programming and offline verification, then fixturing, then roughing, then finishing, then inspection and first-article reporting. Each stage has a way to fail, and the expensive ones are the first and the last.
The manufacturability review is where cost is actually decided. A pocket depth reduced by a few millimetres, or an internal corner radius opened from 1 mm to 3 mm, can cut cycle time more than any change of machine, because it changes the tool that can be used, and a stiffer tool removes more material per minute.
The chain, stage by stage, with the buyer-relevant failure mode for each:
- CAD → manufacturability review — the drawing is checked for tool access and tolerance sanity. Failure: an impossible tolerance quoted as if it were free.
- CAM programming & verification — toolpaths are generated and simulated. Failure: a crash that simulation would have caught.
- Setup & fixturing — the part is held and datums set. Failure: a datum chosen for convenience, not repeatability.
- Roughing — most material is removed fast. Failure: heat build-up that moves the part.
- Finishing — final surfaces and dimensions are cut. Failure: tool wear allowed to drift the last pass.
- Inspection & first-article — the part is measured against the drawing. Failure: a report authored from the model instead of the metal.
What does 3 axis CNC machining cost, and what drives it?
Cost is driven by setup time amortised over quantity, cycle time, material and tooling, inspection labour, and the risk premium on the tolerance. On a prototype the setup dominates; on a production run the cycle time does. That is why a per-part price without a quantity is not a price.
The driver buyers most often underestimate is inspection. A drawing that calls out twenty dimensions has a different inspection cost from one that calls out five, and a first-article report has to be authored, not assumed.
Material is a cost driver in its own right, and the whitelist below is what runs cleanly on these floors:
| Material family | Example grades | Machinability note |
|---|---|---|
| Aluminum | 6061, 7075 | High — fast, long tool life, the default for prototypes |
| Steel | 1018, 4140 | Moderate — 4140 is tougher, slower feeds |
| Stainless | 304, 316 | Lower — work-hardens, needs sharp tools |
| Titanium | Grade 2 / 5 / 23 | Low — low conductivity, low speeds, careful heat control |
| Brass / Copper | C360 / C110 | High (brass), moderate (copper — gummy) |
| Engineering plastics | PEEK, Delrin (POM) | High — watch for heat and burrs |
Cost positioning: 3-axis is the cheapest of the CNC milling families per machine-hour because the machines are simpler and the setups are fewer. The trap is treating it as a commodity — the spread between a well-DFM'd part and a poorly one on the same machine can be 2× in cycle time, and that is decided at review, not at quote.
What actually goes wrong, and how is it prevented?
The failures that cost money are not crashes. They are the quiet ones: a tolerance held on the machine but lost in a later operation, a revision built from a superseded drawing, and a surface finish callout that meant something different in another standard.
Each has a cheap control. Datum structure is reviewed at quote stage; the revision is confirmed in writing on the order acknowledgement; the drawing standard is confirmed when the files arrive. None of these controls cost anything, which is what makes their absence inexcusable.
The most common buyer-side mistakes, in order of how often they appear:
- Quoting tolerance as a single number — ±0.003 mm on a 2 mm feature and on a 400 mm feature are different propositions; it must be set per feature.
- Sending a model with no datum structure — the shop has to invent one, and that invention is where tolerance stacks begin.
- Assuming inspection is included — a first-article report is a document someone authors; confirm it is in the quote.
- Confusing "5-axis part" with "complex part" — many "complex" parts are three setups on a 3-axis centre at a fraction of the cost.
What is the certification position?
ISO 9001:2015, IATF 16949:2016 (excluding clause 8.3 product design), and ISO 14001:2015 — each with a certificate number verifiable with the registrar.
The three certificates held by Dongguan Zhuohang Ltd are ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, excluding clause 8.3 product design), and ISO 14001:2015 (116024/B/0001/UK/En). Each carries a number you can verify with the registrar.
What is not held, stated plainly: there is no AS9100, no NADCAP, and no ISO 13485 on this scope. For aerospace or medical work that needs them, that is a hard stop on those specific certifications — the shop does not present itself as certified where it is not. Where a part still needs, for example, third-party ultrasonic testing to ASTM B594, that inspection is routed to an external accredited laboratory and the result is reported back with the part. State the cert requirement up front so the route can be planned, not discovered at first article.
What tolerance applies?
±0.003 mm on CNC milling, ±0.002 mm on CNC turning; ±0.002 mm where precision grinding or wire EDM is used, set feature by feature when we quote.
For context against platform baselines: a common marketplace standard is ±0.005 in (±0.127 mm) per ISO 2768, with a starting surface finish around Ra 125 µin (3.2 µm). The figures above — ±0.003 mm milling and ±0.002 mm turning — are tighter, but they are capability, not a blanket promise: the number that actually applies is set feature by feature from geometry, material, and datum structure at quote time.
Capability promise (threshold, not a measured result): Ppk ≥ 1.67 at PPAP; Cpk ≥ 1.33 at run rate. The index is reported with its phase and its σ method, so you can see whether a number is from a first-article study or from running production — not a single headline figure presented as both.
What this shop actually runs
Capability evidence should come as specifics, not slogans. Behind this guide is a 6,800 m2 plant in Dongguan, China running 100+ CNC machines with 100+ staff. The machine list by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Cut on compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Cut on prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Cut on long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Cut on shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Cut on hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance: ±0.003 mm CNC milling / ±0.002 mm CNC turning / ±0.002 mm grinding and wire EDM. Capability: Ppk >= 1.67 initial on key characteristics, Cpk >= 1.33 ongoing.
Certificates: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, with design clause 8.3 excluded, stated openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, registration 91441900MA4UWT6X39, founded 2005.
Where we ship: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — plus other countries and regions worldwide, shipped from our base in Dongguan, China.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Get a quote with the cost drivers named
Send your drawing to [email protected] or call +86 13126536955. We will tell you which tolerance or setup is driving the number, not just the number.
Frequently Asked Questions
Can you work to ASME Y14.5 as well as ISO?
Yes. Both geometric dimensioning conventions are used. The important thing is that the drawing states which one applies, because the same symbol can mean different things under the two standards.
Do you hold stock or consignment for repeat orders?
Repeat orders can run against a forecast so stock and, where the part warrants it, dedicated fixturing are held ready. This is a commercial arrangement, not a standard term, so raise it at the second order rather than the first.
How long does 3 axis cnc machining take?
Lead time is driven less by cutting time than by queue position, fixture design, and inspection. A part that needs a purpose-built fixture has a longer first-article lead and a much shorter repeat lead, which is worth asking about separately.
Is your IATF 16949 certificate valid for design work?
No. The certificate excludes clause 8.3 (product design). The plant is certified to manufacture to your design and to run the associated process controls, not to originate product design.
What materials do you machine?
Aluminum, stainless steel, titanium, brass, copper, and Inconel for metals; PEEK and Delrin (POM) for plastics. Material certificates are verified on incoming stock.
How is an engineering change handled mid-production?
The change is documented against a revision, the affected parts in process are identified, and the revised drawing is confirmed in writing before work restarts. The important part is that the revision in force at any moment is a single, written one.
How is material traceability maintained?
Incoming stock is checked against the mill certificate — composition by XRF, hardness where specified — and traceability is held per heat or per batch as the certificate defines it.
Continue reading: 4 Axis CNC Machining · 5 Axis CNC Machining
Standards referenced on this page
- ASTM A582/A582M-12 — Standard Specification for Free-Machining Stainless Steel Bars
- ASTM B211/B211M-19 — Standard Specification for Aluminum-Alloy Rolled or Cold Finished Bar, Rod, and Wire
- ISO 9001 — Quality management systems — Requirements