
1. What a 3-axis lathe is
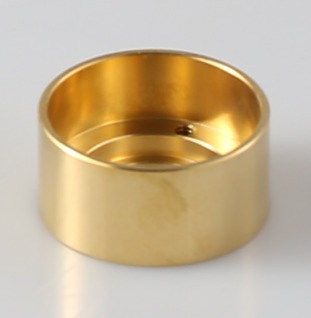
A CNC lathe spins the workpiece on its axis while cutting tools move in to shape it. The two basic axes are Z (along the length of the part) and X (toward and away from the centreline). A "3-axis" lathe adds a C-axis — the spindle can be positioned to a precise angle — so the machine can drill a cross-hole or mill a flat without moving the part to a second operation. That third axis is what lets a lathe do more than just round profiles.
The mental model: a lathe makes round things from round stock. A mill makes shaped things from blocks. If your part is rotationally symmetric, turning is usually faster, tighter and cheaper than milling it from a billet.
2. How turning works in practice
- Chuck and bar feed. The stock is gripped and rotated; for production, bar feeders keep feeding stock so the machine runs unattended.
- Turret tools. Roughing and finishing tools cut diameter and length; the C-axis enables cross-drilling, slotting and light milling.
- Live tooling. Powered tools on the turret cut features off-axis (hex bosses, transverse holes) in the same setup.
- Tolerance advantage. Because the cutting point stays at a fixed radius from the spindle centre, diameter control is often tighter than on a mill.
3. Parts that suit turning
| Part type | Why turning fits |
|---|---|
| Shafts and spindles | Long, round, diametral tolerances |
| Bushings and sleeves | Concentric ID/OD, often with grooves |
| Pins and studs | Small, high-volume, threaded ends |
| Connectors and fittings | Rotationally symmetric, often with cross-holes |
| Threaded fasteners (custom) | Single setup for thread + features |
Turned diameters commonly hold ±0.002 mm (±0.0002 in) on capable equipment. If your part has a flat or a feature that can't be reached by rotating stock, it may need a mill, or a lathe with live tooling to do it in one setup.
4. RFQ checklist for turned parts

- Model plus the stock diameter and material grade (e.g., "Ø20mm 6061-T6 bar").
- Quantities and whether bar feed is viable for volume.
- Critical diameters and their tolerances; mark which are critical-to-function.
- Thread specifications: size, pitch, class, and which end.
- Cross-holes, flats or hex features (these need live tooling / C-axis).
- Surface finish on sealing or bearing surfaces.
5. Common mistakes buyers make
- Designing a "round" part that isn't. A flat or keyway that needs a second op adds setups; ask whether live tooling can absorb it.
- Not specifying stock diameter. Leaving it open lets the shop pick a size that wastes material or can't hold tolerance.
- Over-tolerancing non-critical diameters. Tight specs on every step raise scrap without improving function.
- Forgetting thread class. "M8 thread" is incomplete; class (e.g., 6g/6H) determines fit.
6. How a capable shop approaches turning
A competent turning supplier runs rigid CNC lathes (Brother, Tsugami and similar), uses bar feed for volume, and holds documented process capability so a 10,000-piece reorder matches the first article. At Zhuohang Precision Machining Factory, turning is integrated with milling and grinding under one quality system (ISO 9001, IATF 16949), so a part that is turned and then milled stays in one workflow with one inspection record — fewer hand-offs, fewer chances for misalignment.
What the extra axes actually buy
The axis count is about setups, not precision. A 3-axis machine cuts from one direction, so a part with features on several faces needs to be re-fixtured between operations - and every re-fixture introduces a small error. A 4-axis machine adds rotation, and a 5-axis machine can reach five sides in one setup, so the features on several faces stay in the same coordinate frame and line up. For a part that is a prismatic block, 3-axis is enough and cheapest; for a part with angled or multi-face features, the extra axes buy accuracy and fewer operations. You choose the axis count for the geometry, not by habit.
How to read an axis-based quote
If a part genuinely needs 5-axis work, the quote reflects one setup and tighter feature relationships; if a shop puts a 3-axis part on a 5-axis machine and charges for it, you are paying for capability the geometry does not use. This floor runs 3-, 4- and 5-axis machines including the Mazak VARIAXIS I-600 five-axis and the INTEGREX I-250H S mill-turn, at ±0.003 mm milled. Contact Felipe Iglesias at [email protected] or +86 13126536955 with the drawing and ask which axis count the geometry actually justifies.
How to verify the claim in one email
The fastest way to separate a real floor from a brochure is to ask for the machine list and the certificate numbers - and this facility answers in one email. Dongguan Zhuohang Ltd operates 100+ CNC machines across 6,800 m² in Hengli Town, Dongguan: Mazak VARIAXIS I-600 five-axis, INTEGREX I-250H S mill-turn, Brother SPEEDIO, and TSUGAMI, STAR and CITIZEN Swiss lathes. Inspection is on a Hexagon CMM with the 10:1 gauge rule, certification is to ISO 9001:2015, IATF 16949:2016 and ISO 14001:2015, and critical characteristics run at Ppk 1.67 initial and Cpk 1.33 in production.
Worldwide buyers across Europe, the Americas, Asia, Oceania and Africa are supplied from Dongguan. MOQ is 1 piece, lead times run roughly 3 / 7 / 30 days, and the quote from Felipe Iglesias ([email protected], +86 13126536955) comes back with the routing and the capability evidence together.
Take the next step
One drawing and one quantity is the whole hand-off. Send a STEP or IGES model and a 2D drawing with the tolerances, datums, material grade and finish, state the quantity and lead time, and the reply is an itemised quote - material, setup, cycle time, inspection - rather than a round number. If the drawing is incomplete, send what you have and the open questions; the point is to open the conversation, not to wait for a perfect package.
Contact Felipe Iglesias at [email protected] or +86 13126536955. MOQ is 1 piece, lead times run about 3 / 7 / 30 days, and the service area covers Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa, shipped worldwide from Dongguan.
Tolerance and surface finish reference
±0.003 mm milled, ±0.002 mm turned, and ±0.002 mm ground or wire-cut, all verified on a Hexagon CMM against the datum scheme. Surface finishes span Ra 0.8 to 3.2 µm as-milled, Ra 0.2 to 0.4 µm ground, and Ra 0.05 to 0.1 µm polished. The 10:1 gauge rule governs every feature - the instrument must resolve ten times finer than the tolerance it checks. And the datum is what makes the tolerance real: read against two different datums, the same callout gives two different parts, so state the datum and the convention, ASME Y14.5 or ISO.
The material decision
Aluminium 6061-T6 leads on light and economical; 7075-T6 adds strength for aerospace and structural parts. In stainless, 303 machines cleanly for fittings, 304 and 316 add corrosion resistance, and 17-4 PH adds strength after ageing. Steel wins on strength and cost. Brass is the fastest metal to machine and conducts well. Copper C110 is the conductivity benchmark, with C145 tellurium copper for machinability. Titanium and Inconel hold high-temperature strength but machine slowly and cost more. The material is the biggest lever on price, so it is selected for the service - load, environment, temperature - not by habit, and the grade is named on the drawing so the mill certificate confirms it.
Lathe work, in plain terms
A lathe spins the workpiece and a fixed tool removes material, which is why it is the process for round parts - shafts, pins, bushes, fittings and anything with a turned profile. The lathe holds a tight diameter and a clean concentricity because the part rotates about a single axis, and the tool cuts the same circle on every revolution. That is what makes a turned part accurate in a way a milled part on a round feature is not, and why round parts are almost always quoted as lathe work first.
Workholding and the chuck
The chuck is where a lathe job is won or lost. A three-jaw chuck centres round stock quickly; a collet holds small diameters more accurately; soft jaws are machined to a specific part for repeatable, low-run-out clamping. You do not choose the chuck, but the shop's answer to "how do you hold this part" tells you whether the run-out on the drawing is real or hoped for. This floor turns at ±0.002 mm on Mazak, TSUGAMI, STAR and CITIZEN lathes, with the run-out verified on a Hexagon CMM. Contact Felipe Iglesias at [email protected] or +86 13126536955 with the drawing.
De-risking a first order
Start with a handful of parts to confirm the routing and the tolerance, then scale. The same machines, the same inspection bench and the same certificate numbers apply to a single piece and a production run alike, so a small first batch is the proof that a large one will hold the same numbers.
What this shop actually runs
Capability evidence should come as specifics, not slogans. Behind this guide is a 6,800 m2 plant in Dongguan, China running 100+ CNC machines with 100+ staff. The machine list by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Cut on compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Cut on prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Cut on long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Cut on shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Cut on hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerance: ±0.003 mm CNC milling / ±0.002 mm CNC turning / ±0.002 mm grinding and wire EDM. Capability: Ppk >= 1.67 initial on key characteristics, Cpk >= 1.33 ongoing.
Certificates: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, with design clause 8.3 excluded, stated openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, registration 91441900MA4UWT6X39, founded 2005.
Where we ship: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — plus other countries and regions worldwide, shipped from our base in Dongguan, China.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Next step: Send your turned-part model for a review. See our resources page for RFQ templates.
Frequently Asked Questions
What is a 3-axis lathe?
In short, A CNC lathe rotates the workpiece on its axis (the spindle/C-axis) while tools move in X (toward/away from centre) and Z (along the length). A 3-axis lathe typically adds a C-axis so the part can be indexed to a precise angle, allowing cross-drilling and simple milling without a second operation.
When should I use a lathe instead of a mill?
Turning is the natural choice for rotationally symmetric parts — shafts, bushings, pins, connectors, threaded studs. If the part is round and made from bar stock, turning is usually faster and more accurate than milling it from a block.
What tolerance can CNC turning hold?
Turned diameters commonly hold ±0.002 mm (±0.0002 in) on capable equipment. Diameter control is often tighter than milling because the cutting point stays at a fixed radius from the spindle centre.
What should I put in an RFQ for turned parts?
Send the model, the stock diameter and material grade, quantities, critical diameters and tolerances, thread specifications (size, pitch, class), and any cross-holes or flats that need live tooling. State which dimensions are critical-to-function.
Standards referenced on this page
- ASTM B211/B211M-19 — Standard Specification for Aluminum-Alloy Rolled or Cold Finished Bar, Rod, and Wire
- ASTM A276/A276M-17 — Standard Specification for Stainless Steel Bars and Shapes
- ISO 9001 — Quality management systems — Requirements